
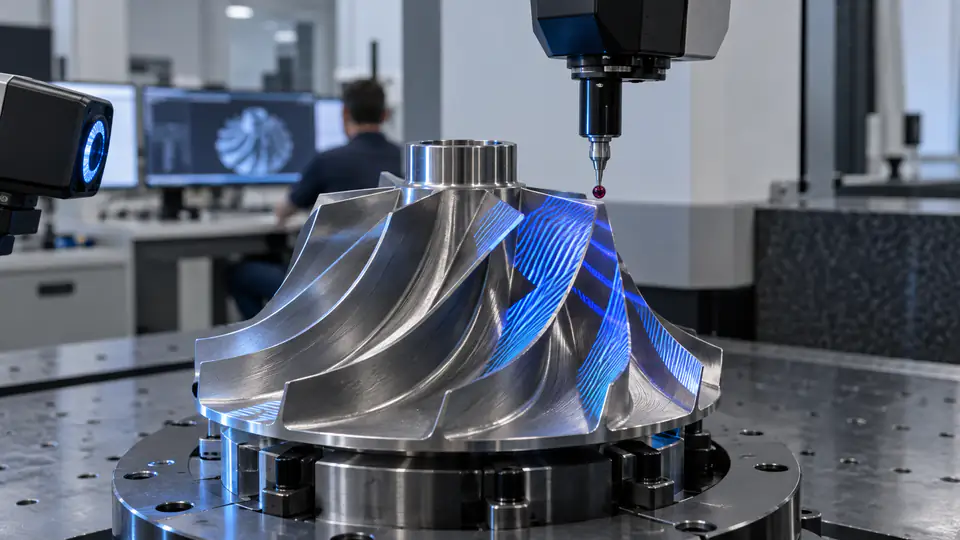
Profile tolerancing can control a contoured CNC surface more clearly than dozens of coordinate dimensions, but only when the nominal geometry, datum frame, tolerance-zone disposition, scope, and inspection method are unambiguous. A feature-control frame attached to an undefined region of a complex model can create more disagreement than it removes.
This profile tolerance CNC surface guide explains how profile of a line and profile of a surface relate to CAD geometry, how datums change the control, how unequal or nonuniform zones should be communicated, and how buyers can plan machining and measurement. It uses general principles; the released drawing must apply the chosen edition of ASME Y14.5 or ISO 1101 and be reviewed by qualified GD&T personnel.
What Profile of a Surface Controls
Profile of a surface establishes a three-dimensional tolerance zone around a theoretically exact surface. Under the governing standard and modifiers, the actual surface must lie within that zone. When related to datums, the control can limit form, orientation, and location. Without datum references, it primarily controls form relative to the true profile under the applicable rules.
This makes profile useful for freeform contours, blended housings, airfoils, ergonomic shapes, sealing surfaces, cast or forged boundaries, and multi-face interfaces. It can control planar and cylindrical surfaces too, although a simpler tolerance may communicate function better.
Do not assume profile means “surface finish.” Profile is a geometric control on shape and location. Roughness, waviness, defects, and coating require separate specifications when needed.
Profile of a Line Versus Profile of a Surface
Profile of a line creates a two-dimensional zone in each defined cross-section or line element. Profile of a surface creates a three-dimensional zone over the specified surface. The line control can suit section-specific requirements, but the drawing must define section orientation and extent.
Use surface profile when the entire spatial contour matters. Use line profile when function is evaluated in defined sections and variation along another direction is handled separately. Do not select line profile merely because the inspection equipment collects line traces; measurement method should verify the product requirement, not redefine it.
| Question | Profile of a line | Profile of a surface |
|---|---|---|
| Tolerance zone | Two-dimensional in defined line elements | Three-dimensional around the nominal surface |
| Typical use | Controlled cross-sections, longitudinal/circumferential elements | Full contoured faces and combined surfaces |
| Drawing need | Define section direction and scope | Define complete surface scope |
| Inspection concern | Enough sections to represent variation | Adequate 3D coverage and accessibility |
The CAD Model Must Define the True Profile
For a complex contour, the basic geometry often resides in the 3D model. The drawing should identify the model revision, authority, units, and surfaces to which profile applies. A PDF view alone cannot recreate an arbitrary freeform surface.
Verify that the supplier imports the same model geometry. Translation repair, loose sewing tolerance, or a different configuration can shift or split faces. Use validation properties, key sections, and geometry comparison where risk warrants it.
If the drawing contains basic dimensions that supplement the model, ensure they do not conflict. Define whether a simplified drawing view is illustrative or authoritative.
Define the Datum Reference Frame
Datums connect the profile zone to functional interfaces. Choose datum features that reproduce how the part is constrained in assembly or use. A stable mounting plane, locating bore, and clocking feature may form a logical frame for a housing. A freeform exterior chosen only because it is easy to scan may not.
The datum sequence matters because it constrains degrees of freedom in order. Material-condition modifiers, datum targets, common datums, and other rules can change simulation. Apply them only when they express real assembly behavior.
The supplier and inspector should be able to describe:
- physical datum features;
- simulators or fixture contacts;
- sequence of establishment;
- any mobility permitted by the standard;
- part state and restraint;
- transformation used by measurement software.
A best-fit alignment is not automatically the drawing datum alignment.
Decide Whether the Zone Is Equally Disposed
A default profile zone is often equally disposed about the true profile under the selected standard. That permits variation on both sides. Function may require more material, less material, or a one-sided boundary.
Examples include maintaining minimum wall, preserving flow area, avoiding interference, retaining machining cleanup on a casting, or controlling a sealing face. Use the standard’s defined notation to specify unequal disposition rather than shifting the CAD model or explaining it only in a supplier email.
Check the entire geometry at transitions. A one-sided zone can conflict with adjacent size, edge, or wall requirements if the drawing is not coordinated.
Use Nonuniform Profile Only with Clear Boundaries
Some surfaces need different tolerance widths by region. A tight sealing band may transition to a wider cosmetic contour; an airfoil may have separate leading-edge and general-surface requirements.
Prefer clear separate zones, surface identifiers, or model annotations. If the governing standard provides nonuniform-zone notation, apply it correctly and show where the variation begins and ends. Avoid a single general note whose limits cannot be mapped to specific CAD faces.
Every transition should be inspectable. A supplier cannot quote “tight near the important area” without a geometric boundary.
Scope the Controlled Surface
A profile callout can apply to one face, a group of connected faces, an all-around boundary, or an entire defined surface set. Make scope visible. CAD face colors or layers can help navigation but require a controlled legend and a neutral exchange that preserves them.
Do not unintentionally include holes, threads, chamfers, parting lines, edge breaks, or masked areas. Define exclusions and separate controls. At tangential blends, state whether the surface group must be continuous or whether individual faces are evaluated independently.
For a composite outer housing, divide functional, cosmetic, and noncritical regions rather than applying one expensive tolerance to every pocket and relief.
Relate Profile to Size
Profile is not a universal substitute for size tolerances on every feature of size. A width, diameter, or thickness may need separate size control under the governing standard. The profile zone can also limit surfaces contributing to that feature, creating combined effects that must be reviewed.
For a thin wall between two profiled surfaces, worst-case thickness depends on disposition and correlation. Explicitly protect minimum wall where pressure, stiffness, or machining breakout matters. Do not assume two independent profile callouts preserve thickness.
Review mating clearances and envelopes at worst case rather than nominal CAD only.
Use Composite Profile for Different Functions
Composite profile can refine relationships within a pattern or surface set while allowing a broader relationship to the datum frame, depending on the governing standard. It can be useful when overall location has one tolerance but local feature-to-feature relationship needs tighter control.
This is advanced notation and is frequently misread. The design team should document the functional purpose of each segment and confirm interpretation with manufacturing and inspection before release. If the requirement can be expressed more simply with separate controls, simplicity may reduce risk.
Do not imitate a composite frame from an unrelated drawing.
Consider Material Boundaries and Coating
Profile should identify the surface state. Coating, plating, polishing, heat treatment, and assembly can change the contour. State whether the control applies before finish, after finish, or to a substrate and coating combination.
For a coated surface, consider thickness variation and measurement method. If the design controls the final external boundary, the machine supplier may need a qualified prefinish offset. Avoid applying the full coating thickness independently to both CAD nominal and machining allowance.
For cast or forged blanks, separate the raw-boundary requirement from the finish-machined surface and define required cleanup or minimum stock.
Design the Machining Strategy Around Surface Sensitivity
Freeform contour accuracy depends on tool geometry, toolpath tolerance, stepover, interpolation, machine kinematics, workholding, thermal behavior, cutter deflection, and stock condition. A smaller CAM tolerance alone does not guarantee a better part.
The supplier should identify:
- roughing and finishing sequence;
- tool type, radius, and effective contact region;
- five-axis or three-axis access and orientation changes;
- fixture and datum transfer;
- toolpath tolerance and smoothing approach;
- expected scallop and surface texture;
- in-process verification or stock mapping;
- areas with limited tool access.
The drawing should specify result, not proprietary toolpath details, unless a validated process requires them.
Understand Chordal and Scallop Effects
CAM systems approximate surfaces into tool motion within chosen tolerances, and finishing leaves cusp or scallop between passes. Machine controllers further interpolate commanded paths. These values influence form and texture but are not interchangeable with the profile tolerance.
A toolpath chordal tolerance should be comfortably inside the manufacturing allocation after considering all other errors. Stepover should meet the required functional texture and visual outcome. Extremely small settings increase code size and cycle time and may expose machine dynamics without improving usable accuracy.
Validate the real surface rather than quoting software settings as conformance evidence.
Protect Thin or Flexible Contours
Clamping force can distort thin shells and leave them out of profile when released. Cutting force, residual stress, heat, coating, and gravity can also change shape.
Define whether the profile applies free-state, restrained, or assembled. For a restrained condition, specify datum simulators, contacts, force or fastener torque, and sequence. The measurement fixture should not mask a nonconforming free-state requirement.
The design can support stable manufacturing through uniform walls, accessible support lands, smooth thickness transitions, and tolerances tied to functional regions.
Plan CMM Inspection
A CMM can compare measured points with CAD nominal under the drawing datum alignment. The plan should define coverage, probe type, point distribution or scanning path, filtering where applicable, alignment, and reporting.
Sparse points may miss local peaks. Dense scanning can still miss inaccessible undercuts or deep narrow channels. Probe radius, stylus bending, surface finish, speed, temperature, and fixture affect results.
Agree on the evaluation algorithm and whether each point must lie within the zone. A colored deviation map is useful visualization, but the report should preserve numeric limits, actual extrema, surface IDs, datum setup, and result.
Use Optical Scanning Carefully
Structured-light and laser scanning can collect dense surface data quickly. Reflective, transparent, dark, deep, or sharp geometry may create missing or biased points. Temporary spray can alter the measured surface and may be prohibited.
Qualify the scanner for the material, size, tolerance, and feature. Establish scale, calibration, alignment, filtering, smoothing, mesh generation, and treatment of outliers. A best-fit color map can hide location error relative to functional datums.
Correlate optical results with a traceable reference or another method on representative geometry. NIST work on freeform/aspheric measurement illustrates that uncertainty in profile reconstruction deserves explicit evaluation.
Define the Data Analysis
Inspection software can align and compare the same point cloud in different ways. Specify datum alignment rather than unconstrained best fit. Define whether nominal comparison is normal to the CAD surface, along a coordinate direction, or by another approved method.
State treatment of:
- edge exclusion;
- holes and discontinuities;
- outliers and invalid points;
- smoothing and filters;
- mesh decimation;
- temperature compensation;
- inaccessible areas;
- uncertainty and decision rule.
Preserve raw or minimally processed data when high-risk results may need reanalysis.
Inspect Inaccessible Surfaces
Internal contours may not be reachable by conventional probes or scanners. Options can include sectional templates, replica methods, borescopes, ultrasound, radiography or CT, destructive sectioning of samples, process-qualified tooling, or functional testing.
Each method has limitations. CT dimensional results depend on material, thickness, resolution, reconstruction, calibration, and uncertainty. A visual borescope cannot establish a tight geometric profile.
Address accessibility before releasing a tolerance. If direct verification is impossible, engineering must decide whether to redesign access, use an indirect control, qualify the process, or accept destructive sampling.
Correlate Supplier and Buyer Results
Before production, inspect the same pilot part using the intended methods. Compare datum simulation, support, point coverage, filters, algorithms, temperature, and uncertainty. Resolve differences while the part is available to both parties.
Do not compare only reported pass/fail. Exchange actual values and selected raw data. A supplier and buyer can both be internally repeatable yet disagree because one uses best fit and the other uses datum alignment.
Record the agreed method in the inspection plan and update it with the drawing revision.
Build a Quote-Ready Profile Requirement
Include:
| RFQ item | Required definition |
|---|---|
| Nominal geometry | Controlled CAD file, revision, units, and authority |
| Surface scope | Identified faces, boundaries, and exclusions |
| Tolerance | Value, standard, profile type, and zone disposition |
| Datum frame | Datum features, sequence, modifiers, and targets |
| Part state | Free/restrained, temperature, pre/post finish |
| Inspection | Method, coverage, alignment, analysis, and actual data |
| Sampling | First article, production coverage, and escalation |
| Records | Deviation map, extrema, raw-data retention, approvals |
Ask the supplier to identify unreachable regions, ambiguous transitions, translation issues, and anticipated method differences before quoting.
Common Profile Failures
Inspection uses best fit instead of the datum frame
Reanalyze with the drawing datum simulation and assess affected product. Correct the measurement plan and software template.
The callout does not identify which faces it controls
Issue a marked surface map or model annotation under revision control. Do not let each supplier create its own scope.
A tight profile is applied to hidden nonfunctional geometry
Separate functional zones and relax irrelevant regions. Preserve minimum wall and clearance requirements explicitly.
Scan data looks smooth but misses a local defect
Review point spacing, line of sight, filters, smoothing, edge exclusion, and raw data. Add targeted measurement where risk is concentrated.
Coating causes the final profile to fail
Define final-state authority and qualify the prefinish offset, coating thickness distribution, masking, and post-finish measurement.
Apply Profile to Common CNC Scenarios
Blended housing exterior
Use the model to define the connected contour and identify which faces are cosmetic, mating, or clearance only. A datum-referenced surface profile can locate the exterior to mounting features, while separate texture and visual criteria control appearance. Exclude logos, threaded holes, and edge breaks unless their inclusion is deliberate. Inspection should sample high-curvature blends and transition zones, not only broad easy-to-scan faces.
Sealing groove or land
Protect the relationship between the sealing path and its functional datums. Profile may control a complex land, but groove width, depth, surface texture, scratches, and minimum wall can need separate limits. Evaluate the final finish state and the seal’s real contact band. A global best fit is inappropriate when leakage depends on location relative to ports and fasteners.
Turbine, compressor, or fan blade
Different regions may have different sensitivities. Leading edge, trailing edge, pressure surface, suction surface, platform, and root interfaces can need separate zones and sampling density. Coordinate the profile with thickness, edge radius, surface texture, and balance requirements. Define sections and datum frame from the part’s assembly function. Do not infer an allowable blend from a colored scan alone.
Ergonomic or visible product shell
The outer shape may be controlled loosely for fit and tightly for visible continuity in selected regions. Separate geometry from gloss, texture, and scratch criteria. If the shell is thin, define free and assembled states. A surface profile that is unnecessarily tight everywhere can increase machining and inspection cost without improving what the user sees or touches.
Cast or forged blank with machined pads
Use profile to control the raw boundary where stock, clearance, or wall matters, and separate controls for finished pads and bores. Define datum strategy that survives both blank and machining stages. Unequal disposition may protect minimum machining stock, but the notation and inspection method must follow the governing standard. Coordinate the blank supplier and machine shop so both evaluate the same nominal model.
Questions Buyers Often Ask
Does profile replace plus/minus dimensions?
It can replace many coordinate dimensions used to locate a contour, but it does not automatically replace every size, thickness, radius, texture, or interface requirement. Review feature-of-size rules and worst-case boundaries under the selected standard. Keep separate requirements when they express a different functional decision.
Can the supplier use best fit for process control?
Best fit may help diagnose machining form or stock distribution, but product acceptance must use the drawing-defined datum alignment unless another method is explicitly authorized. Reports should label diagnostic best-fit results so they cannot be mistaken for acceptance data.
How many scan points are enough?
There is no universal count. Density should resolve the smallest relevant deviation considering surface curvature, machining wavelength, probe or optical spot, and risk. Use additional points near sharp curvature, blends, edges, tool transitions, and known process sensitivities. Validate the plan with representative defects or comparison measurements.
Is a color map sufficient evidence?
No. It should be accompanied by part and revision identity, datum alignment, nominal model, units, tolerance limits, scale, coverage, filters, extrema, inaccessible zones, and disposition. Preserve the numeric data required to reproduce or challenge the result.
Should the profile value equal the process capability?
The design tolerance should follow function and assembly. The supplier then demonstrates a manufacturing and measurement process capable of supporting that tolerance with suitable margin. Do not widen a functional limit merely to match one process, and do not tighten the drawing to a hoped-for machine specification without product need.
Final Design and RFQ Checklist
Before release, verify that:
- the correct GD&T standard and edition are specified;
- the controlled CAD defines true profile;
- line versus surface profile is intentional;
- datum features represent functional constraint;
- surface scope and exclusions are unambiguous;
- zone disposition and any nonuniform regions are defined;
- size, wall, clearance, texture, and coating needs are separately protected;
- free or restrained inspection state is reproducible;
- machining access and toolpath strategy are feasible;
- measurement coverage can find relevant deviations;
- alignment, filtering, outlier, and reporting rules are agreed;
- supplier and buyer methods are correlated where risk warrants it.
Make the Tolerance Match the Function and the Measurement
Profile tolerancing is powerful because it can connect a complex nominal surface to functional datums in one coherent control. That power depends on a complete CAD authority, precise scope, correct zone, feasible manufacturing, and a measurement plan that applies the same interpretation.
Send QuickCNCs the controlled 3D model and 2D drawing with datum strategy, surface map, material, finish, quantities, and inspection requirements. The team can review contour access, five-axis strategy, fixturing, and metrology through CNC milling services and precision CNC machining. Submit the package through Request a Quote.
References
- ASME Y14.5 Dimensioning and Tolerancing — GD&T rules and profile-tolerance guidance.
- ISO 1101:2017 — geometrical tolerancing language for form, orientation, location, and run-out.
- NIST uncertainties in aspheric profile measurements — uncertainty considerations for reconstructed freeform profiles.