
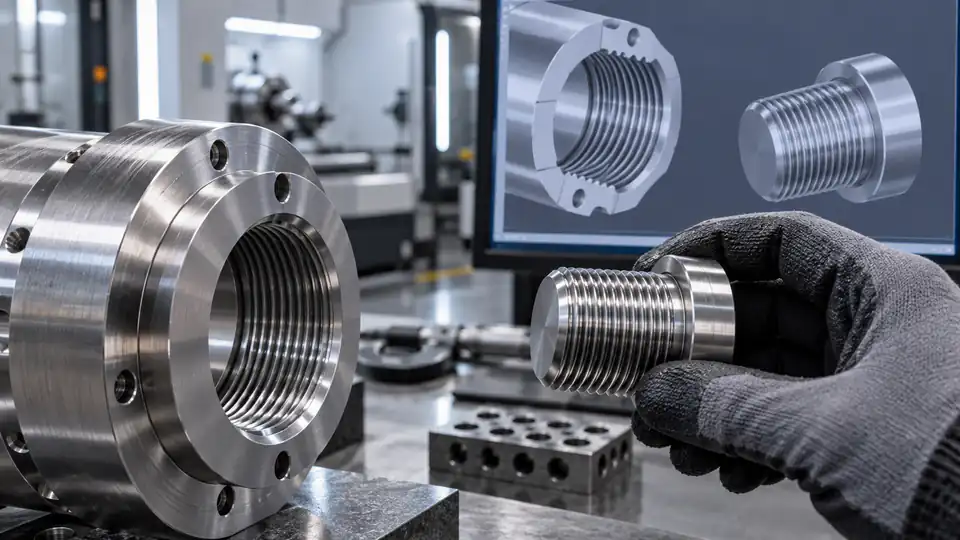
A helical shape in a CAD model does not fully specify a production screw thread. The model may contain a cosmetic representation, a simplified cylinder, an exact nominal profile, or geometry altered for rendering or additive manufacture. It rarely communicates every item a machinist and inspector need: thread standard, size, pitch, tolerance class, handedness, engagement length, entry, runout, coating state, gaging, and acceptance.
This modeled threads vs drawing threads CNC guide explains how to divide authority between 3D geometry and the released callout, when full thread modeling is useful, how to prepare a CNC RFQ, and how to avoid double-counting clearance or coating allowance. The governing drawing, standard, and mating-part design remain the authority for each real product.
Clear authority prevents avoidable manufacturing, assembly, inspection, and supplier-communication errors.
What a Thread Callout Defines
A complete standard-thread designation points to an established profile and tolerance system. ASME B1.1 covers unified inch thread forms, series, classes, allowances, tolerances, and designations. ISO 965 provides the tolerance system for ISO general-purpose metric threads. Product-specific, aerospace, pipe, insert, tapered, or custom threads may use other standards.
The RFQ should identify as applicable:
- thread standard and edition;
- nominal diameter and pitch or threads per inch;
- internal or external thread;
- tolerance class;
- right-hand or left-hand direction;
- number of starts for a multistart thread;
- full or usable thread depth/length;
- through or blind condition;
- entry chamfer, countersink, spotface, or relief;
- runout and incomplete-thread allowance;
- final coating or plating state;
- gaging or measurement requirement.
The modeled helix can support understanding, but it does not replace this controlled language.
Recognize Common CAD Thread Representations
CAD systems generally represent threads in one of four ways:
| Representation | What the supplier sees | Appropriate use | Main risk |
|---|---|---|---|
| Cosmetic metadata | Cylinder plus thread annotation/property | Normal design and drawing workflows | Metadata may not transfer to neutral CAD |
| Simplified geometry | Major/minor diameter approximation | Clearance, visualization, lightweight models | May be mistaken for actual cutting geometry |
| Fully modeled nominal helix | Explicit flanks and root/crest shape | Rendering, interference, special manufacturing analysis | Nominal geometry omits tolerance and manufacturing details |
| Custom functional geometry | Explicit nonstandard profile and lead | Special threads, worms, feed screws | Requires complete tolerance and inspection definition |
Before quoting, the supplier should determine which representation was provided. Do not calculate a thread from a measured cylinder without the callout.
Let the Drawing Control Standard Threads
For ordinary tapped and external machine threads, use the standard designation and dimensions necessary to locate the feature. The 3D model may show a cosmetic or simplified thread to keep file size manageable and avoid fragile helical topology.
State the model/drawing conflict rule. A practical rule is that the model defines nominal part geometry except standard-thread form, which is governed by the drawing callout and cited standard. The drawing also controls thread depth, class, finish state, and gaging.
If the model shows a nominal pilot cylinder, identify whether it represents tap-drill size, minor diameter, major diameter, or only a schematic feature. Many shops ignore cosmetic thread cylinders and generate tooling from the callout; that is safe only when authority is explicit.
Use Fully Modeled Threads for a Defined Reason
Full modeling can be useful for:
- custom thread forms not defined by a standard;
- interference and engagement studies;
- additive manufacturing or molding where the surface is directly reproduced;
- flow or contact analysis that needs helical geometry;
- visualization of interrupted, partial, tapered, or multi-start features;
- collision review near thin walls and adjacent features.
Even then, add tolerances and inspection requirements. The CAD surface is usually nominal. A CAM system can follow it exactly and still create a thread with the wrong allowance, fit, or tool compensation.
Avoid modeling every standard thread in a large assembly without purpose. It increases file size, regeneration time, tessellation, and translation complexity and can create thousands of small faces irrelevant to CNC programming.
Define Thread Depth Correctly
Blind threads need separate definitions for usable full thread, tap or tool travel, drill-point depth, bottom clearance, and entry. A note such as “M6 × 1 THRU 12 DEEP” can be interpreted differently unless the drawing convention is clear.
Ask what function needs engagement. Full-form engagement length is different from total drilled depth. Cutting taps need room for chamfer and chips; forming taps have different preparation; thread milling needs entry and runout. Bottoming near a thin wall increases risk.
Dimension the minimum usable thread needed by the fastener and load, then allow the supplier a feasible tool and drill envelope. Show a section when the bottom geometry is important.
Specify Through Threads and Breakout
A through thread should identify the material thickness and any exit condition. The tool must pass sufficiently to create full form, but breakout can leave a burr or raise an edge on the far surface.
State deburr and chamfer requirements on both sides. If the exit is inside a clean, sealing, cosmetic, or inaccessible cavity, call it out specifically. For a hole intersecting another passage, define acceptable incomplete thread and burr removal.
Do not assume a THRU note authorizes damage to an opposing feature or wall.
Control Thread Location and Orientation
The thread designation controls the helical feature; separate dimensions and GD&T locate its axis and entry surface. For an assembly-critical thread, position may apply to the pitch-cylinder axis according to the chosen standard and drawing practice.
Avoid locating a tapped hole only from a modeled minor cylinder if the drawing uses a different datum scheme. Define the datum reference frame and basic location. For angled threads, include orientation and surface relationship.
Where a bolt pattern locates another component by clearance rather than thread axes, control the functional interface accordingly. Do not over-tolerance every thread because it appears precise in CAD.
Specify Tolerance Class and Fit
Nominal diameter and pitch do not define fit. Unified and ISO metric systems use tolerance classes for internal and external threads. Select the pairing from function, manufacturing process, coating, temperature, assembly, and governing standard.
A tighter class can increase tool, gage, and process-control cost and may be inappropriate after thick coating. A looser class is not a universal solution because engagement and strength still matter.
State whether the final thread must accept a standard mating fastener, a custom counterpart, or a particular gage. For custom pairs, analyze pitch diameter, flank contact, root/crest clearance, lead, and engagement rather than relying on a nominal CAD fit.
Account for Coating and Plating
Coating on thread flanks changes effective size. Anodizing, plating, paint, dry-film lubricant, and conversion coatings behave differently. Some specifications define pre-coating allowance or post-coating class; others require masking, chasing, or final gaging.
Define:
- finish type and thickness range;
- whether threads are coated, masked, or machined after finish;
- required final tolerance class;
- gaging state;
- whether thread chasing is allowed;
- exposed-substrate and corrosion requirements;
- lubricant or locking-compound compatibility.
Do not offset both the model and the tool for coating without a controlled calculation. That can double the allowance.
Design Thread Entries
An entry chamfer helps starting, protects the first thread, and supports gaging. Its size must fit the wall, counterbore, spotface, seal, or cosmetic surface. A large generic chamfer can reduce engagement or break into an adjacent edge.
For external threads, control the lead-in and end relief as needed. A thread that runs to a shoulder may need a relief or an allowed incomplete region. The mating component and assembly tool require access.
Model the entry where it affects adjacent geometry, but dimension or call it out so manufacturing does not infer the requirement from a shaded edge.
Handle Thread Runout and Relief
Cutting tools cannot always produce full form to a shoulder or blind bottom. Thread runout is the transition from full form to incomplete thread. The assembly must keep the mating component out of that region or provide relief.
For shafts, a standard or custom undercut may protect seating and tool clearance but reduces section area and can affect fatigue. For internal threads, counterbores or increased drilled depth can provide tool clearance.
Specify usable engagement, shoulder seating, and relief geometry from function. Let the supplier propose the tool approach unless a standardized interface requires a mandated detail.
Choose Tapping, Thread Milling, or Turning Intentionally
Tapping is efficient for common internal sizes and sufficient access. Thread milling offers flexibility, lower cutting load in some conditions, controllable diameter, and easier recovery from tool breakage, but requires circular interpolation and adequate bore access. Single-point turning suits many external and internal rotational threads. Form tapping displaces material and has specific material, hole-preparation, lubrication, and surface-integrity considerations.
The drawing usually should not mandate the process. Provide thread standard, class, depth, material, quantity, access, and final condition. The supplier can select the method and state any required design change.
Mandate a process only when validated product requirements justify it.
Prepare the Pilot Hole and Wall
Internal-thread strength, forming behavior, and tool load depend on the prepared hole. Do not treat a modeled nominal minor diameter as an automatic drill size. The supplier should use the thread standard, material, process, tool guidance, and desired engagement.
Check remaining wall to adjacent holes, pockets, edges, and channels using worst-case thread and location conditions. A CAD cylinder may not show the real root envelope or drill point.
For tapered pipe or special sealing threads, follow the applicable standard and include boss geometry, engagement reference, sealant, pressure, and inspection. Do not substitute a straight modeled hole.
Address Inserts
Wire, solid, key-locking, self-tapping, and other inserts use specific parent threads, preparation, installation, and inspection. Identify insert manufacturer or governing specification, size, material, locking style, installed depth, tang handling, and final gaging.
The CAD model may show the nominal finished internal thread but omit the larger parent thread and installation feature. State whether the CNC supplier installs the insert or ships the parent thread only.
For blind holes, check tool depth, insert length, tang or drive feature, and bottom clearance. Define proof or torque tests only when required by the product plan.
Inspect Standard Threads
Go/no-go gages provide a functional acceptance method for many standard threads when used under the applicable standard and calibrated control. They do not provide an actual pitch-diameter value or diagnose every error.
Depending on risk and thread type, inspection may include:
- plug or ring gaging;
- pitch-diameter measurement;
- three-wire or two-ball methods for external or internal features;
- lead and flank-angle measurement;
- optical or contour inspection;
- CMM or specialized measurement for large/custom threads;
- torque, engagement, or functional assembly tests.
NIST has published work on pitch-diameter measurement of threaded gages using CMMs, illustrating that thread metrology is a defined measurement problem, not a visual check.
Define Gaging State and Frequency
State whether gaging occurs before or after coating, cleaning, lubrication, insert installation, heat treatment, or assembly. A prefinish pass does not establish final fit if the process changes the flanks.
Define lot and sampling. Critical threads may receive 100% functional gaging; stable repeat work may use controlled sampling plus in-process tool monitoring. Large, fragile, coated, or custom threads may require an alternative method.
Record gage ID, calibration status, part/lot, result, and actual data when required. Do not force a go gage through contamination or coating buildup and then call the thread conforming.
Inspect Depth and Location Separately
A thread gage can show functional fit without proving usable depth or axis location. Verify depth with a suitable method, considering incomplete lead threads and gage nose. Verify location and orientation against the drawing datum system.
For blind holes, also verify drill-point clearance where breakthrough would be unacceptable. For fastener seating, inspect spotface or counterbore geometry and perpendicularity as appropriate.
Use a ballooned inspection plan so each requirement maps to a record rather than one generic “thread OK” result.
Prepare a Quote-Ready Thread Table
For parts with many threads, include a controlled table:
| Field | Buyer definition |
|---|---|
| Feature ID | Drawing or PMI characteristic identifier |
| Designation | Standard, size/pitch, class, hand, starts |
| Quantity | Number of identical features |
| Location | Datum-based basic or coordinate definition |
| Engagement | Minimum full thread or usable length |
| Entry/end | Chamfer, countersink, relief, through/blind state |
| Finish | Coated, masked, post-machined, final class |
| Inspection | Gage/method, coverage, actual data if required |
| Special condition | Insert, locking, sealing, cleanliness, proof test |
Keep the table synchronized with the model and drawing revision.
Define Custom Threads as Complete Geometry
A custom thread needs more than an unconventional diameter and pitch. Define the axial profile, flank angles, crest and root truncation or radius, lead, number of starts, hand, taper if any, pitch diameter or other size basis, tolerances, runout, surface finish, and engagement. Identify the mating component and which side controls each clearance.
For a lead screw, worm, optical adjustment, closure, or fluid interface, include functional conditions such as backlash, contact pattern, travel, load, lubrication, sealing, or self-locking behavior. The geometric model can be authoritative for nominal form only if the release says so and the receiving system can reproduce it accurately.
Agree on manufacturing and inspection before freezing the profile. A form tool, thread mill, whirling process, grinding operation, EDM route, or single-point tool may impose different relief and access requirements. A custom profile that cannot be measured with available equipment is not production-ready.
Supply a sectioned detail and mathematical definition where appropriate. For a periodic profile, identify the axial reference and how cumulative lead error is controlled over the engagement. Use a master, mating gage, or functional test only with controlled identity, calibration or qualification, and a clear wear/replacement plan.
Evaluate the Complete Fastened Joint
Thread fit is one contributor to a joint. Clamp load also depends on fastener material and condition, bearing surfaces, torque or tension method, lubrication, washers, joint stiffness, embedment, and engagement. Do not tighten the thread class in an attempt to solve an uncontrolled preload problem.
Check that the screw cannot bottom in a blind hole before the joint clamps. Confirm clearance under the head, counterbore depth, spotface flatness, tool access, and installation orientation. If prevailing torque, locking patch, adhesive, safety wire, or a mechanical lock is required, define it separately and validate compatibility with finish and service temperature.
For frequently serviced joints, consider wear, galling, corrosion, cross-threading, and replaceability. Inserts may protect a soft parent material, but they introduce installation depth, tang, locking, and traceability decisions. For a permanent high-load joint, calculate engaged thread strength using the actual materials and load distribution rather than counting modeled turns visually.
Where fastener failure affects safety, use the product’s approved design and verification process. This article does not supply torque values or engagement ratios because those depend on the complete joint.
Prevent Chips, Burrs, and Fluid from Hiding in Threads
Blind threaded holes can retain chips, tap fragments, abrasive, cutting fluid, plating solution, and cleaning residue. The drawing and process plan should include access for cleaning and an inspection state free of material that masks gage behavior.
Use appropriate flushing, brushing, air or vacuum methods under controlled safety practices. Confirm cleanliness around intersecting passages and bottom features with suitable visual or borescope inspection. A go gage can push soft debris deeper or temporarily compress contamination without proving the hole is ready for assembly.
If the part enters a cleanroom, vacuum, fluid, medical, or optical system, define the permitted residue and verification method. Cap or bag the cleaned thread so packaging does not reintroduce fibers or particles. Ensure temporary plugs are counted and removed at the correct assembly step.
Review deburring at both entry and exit under suitable magnification. A rolled burr can let a gage start yet damage a production fastener, while aggressive hand blending can remove the first full thread or enlarge a sealing chamfer. Tie the edge treatment to the same characteristic ID as the thread when the conditions interact, and preserve photographic evidence only where it supports the defined visual method.
Common Failure Modes
CAM cuts the modeled nominal helix directly
Stop and compare the geometry with the governing thread standard, class, and allowance. Regenerate the operation from the controlled callout unless the modeled custom profile is explicitly authoritative.
A thread passes before plating and fails afterward
Review thickness on flanks, pre-plate allowance, masking, final class, and gaging state. Correct the released finishing strategy rather than hand-working every part without approval.
The screw bottoms before the joint clamps
Compare usable thread, screw length, blind-hole depth, runout, debris, and stack-up. A depth note may have described drill depth instead of full-thread engagement.
The thread gage passes but the fastener pattern does not assemble
Inspect axis position, orientation, datum alignment, counterbores, mating-part variation, and fastener clearance. Gage fit and feature location are separate decisions.
A neutral model loses cosmetic thread data
Use the controlled drawing or validated PMI as authority. Do not infer size from the imported cylinder.
Final RFQ Checklist
Before release, verify that:
- every thread has a standard or complete custom definition;
- size, pitch, class, hand, starts, and internal/external state are clear;
- usable engagement is distinguished from drill/tool depth;
- through exits, blind bottoms, chamfers, and reliefs are defined;
- axes are located and oriented from functional datums;
- coating and plating allowance is applied once and verified in final state;
- modeled geometry has a stated role;
- neutral-file loss of cosmetic metadata cannot change the order;
- inserts include type, installation, and inspection requirements;
- gaging method, state, sampling, and records are specified;
- depth and location are inspected separately from functional fit;
- the supplier has raised access or manufacturability exceptions before award.
Use the Model for Geometry and the Callout for Authority
Full helical modeling can support analysis and special geometry, but most standard CNC threads are safer and lighter when the released callout controls their form and tolerance. The supplier should never need to measure a rendered helix to discover what fastener fits.
Send the neutral 3D model and controlled 2D drawing with thread table, finish state, quantities, material, and inspection needs. QuickCNCs can review access, engagement, machining method, coating allowance, and gaging through CNC milling services and CNC turning services. Submit the complete package through Request a Quote.
References
- ASME B1.1: Unified Inch Screw Threads — unified inch thread forms, series, classes, allowances, tolerances, and designations.
- ISO 965-1:2026 — tolerance system for ISO general-purpose metric screw threads.
- NIST pitch-diameter measurement of threaded gages — dimensional-metrology research for screw-thread pitch diameter.