
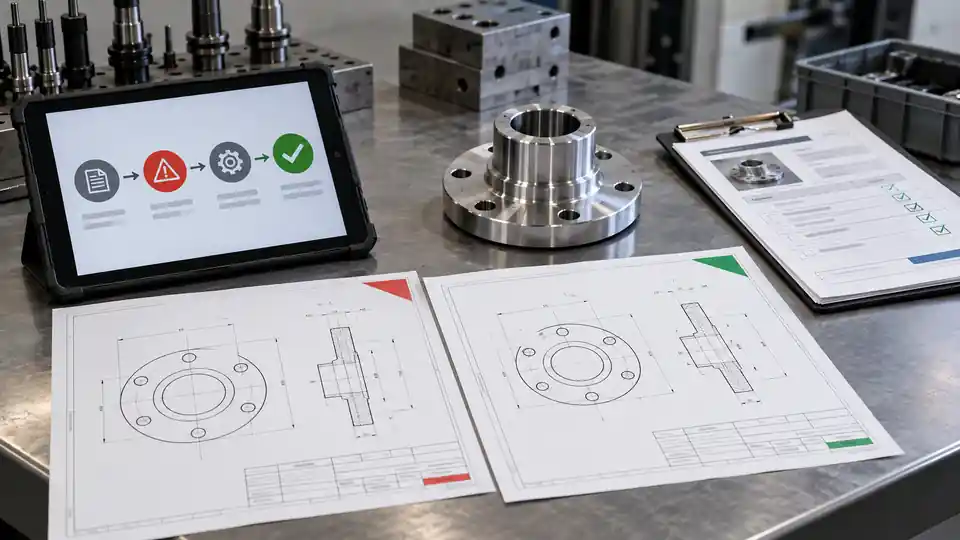
A revision is not controlled merely because a supplier received a new PDF. The change has to reach quoting, planning, programming, purchasing, machining, outside processing, inspection, packaging, and shipment release at the correct effectivity. Obsolete models, drawings, setup sheets, CMM programs, or sub-tier instructions can remain in use long after an email was acknowledged.
This CNC supplier revision communication inspection checklist is designed for a buyer auditing that end-to-end process. It tests how a supplier receives, compares, approves, distributes, implements, and proves a product-definition change. It also separates supplier workflow from customer authority: the supplier may plan implementation, but only the authorized product owner can approve deviations or define which revision is contractually effective.
Define the Controlled Product Package
Start by listing every item that can define or affect the ordered product. A revision audit fails if it follows the drawing but ignores the model, purchase order, specification, or approved change notice.
The controlled package may include:
- 3D CAD model and native/neutral file identity;
- 2D drawing and revision;
- parts list or bill of material;
- customer and industry specifications;
- material, finish, and special-process requirements;
- quality clauses and inspection plan;
- approved deviations, waivers, or concessions;
- packaging, marking, and labeling requirements;
- digital product definition or PMI rules;
- purchase-order revision and line-item notes; and
- effective serial, lot, work order, or date.
For each source, identify the owner and conflict rule. If the model and drawing disagree, the supplier must not decide which wins from habit. The order should state the authority or require formal clarification.
Audit the Change From Customer Release to Shipment
Select one real, completed revision and trace it through the supplier’s records. Policy alone shows intended practice; the audit sample shows operation. Prefer a change that affected geometry, material, inspection, or outside processing rather than an editorial correction.
Build a timeline:
- customer issued the change;
- supplier received and logged it;
- responsible functions reviewed impact;
- clarification or approval closed;
- open inventory and work in process were dispositioned;
- programs, routers, fixtures, and inspection documents were updated;
- subtiers received and acknowledged applicable changes;
- first effective product was verified; and
- shipment records proved the implemented revision.
Compare timestamps and identities. A CMM program updated after the first revised lot shipped is a concrete gap even if the document-control procedure looks strong.
Verify the Intake Channel
Ask how the supplier recognizes an authorized change. Email, portal download, EDI, PLM connection, or revised purchase order may be accepted channels. Personal messages, chat attachments, and verbal requests should not silently become product authority.
Review controls for:
- approved customer contacts and portals;
- secure receipt and malware scanning;
- file naming and unique identifiers;
- receipt timestamp and responsible owner;
- checksum or revision comparison where useful;
- acknowledgment to the customer;
- duplicate or conflicting transmittals; and
- failed downloads or unreadable files.
An acknowledgment should mean more than “email received.” Distinguish receipt, technical review, commercial acceptance, and implementation readiness. The customer should know which state has been reached.
Emergency or verbal changes
Urgent production issues tempt teams to accept a screenshot or phone instruction. Define a temporary containment path and a deadline for controlled written authorization. Record who approved the interim action, affected units, and expiration. If formal authority never arrives, stop rather than normalizing the exception.
Confirm Exact Revision Identity
The supplier should record part number, document number, revision, file name, date, and an immutable file identifier or controlled repository version. “Latest file” is not enough. A neutral CAD model can retain the same visible part name while geometry changes.
Compare the released model and drawing with the supplier’s stored master. Open files and verify internal metadata, units, coordinate system, suppressed features, external references, assembly structure, and export information. When practical, use controlled geometry comparison to find changed faces or dimensions.
Do not rely solely on modification timestamps; copying or downloading can alter them. Use the customer’s transmittal, PLM identifier, revision field, or cryptographic hash according to the agreed process.
Require a Technical Change Review
Every revision should be classified by actual effect. A title-block change may have no process impact, while a one-line material or finish change can affect stock, tooling, inspection, lead time, and cost.
The review should consider:
- geometry and tolerances;
- datum scheme and measurement method;
- material grade, condition, and product form;
- surface finish, coating, masking, and dimensional growth;
- special processes and approved sources;
- setup count, workholding, tooling, and tool access;
- CNC and CMM program changes;
- purchased components and subtiers;
- work in process and finished inventory;
- first-article or validation requirements;
- capacity, price, and delivery impact; and
- regulatory or customer approvals.
Record “no impact” with a reason. A checkbox without analysis is weak evidence.
Establish Effectivity Before Implementation
Revision identity tells what changed; effectivity tells where the change begins. Use an unambiguous boundary: serial number, lot, work order, production date/time, shipment, or purchase-order release.
Avoid “use new revision as soon as possible.” Different departments will interpret it differently. The supplier needs to know whether existing raw material, in-process parts, finished stock, replacement parts, and sub-tier orders may be used.
| Population | Decision to document | Typical evidence |
|---|---|---|
| Uncut raw material | Continue, reallocate, return, or scrap | Material/PO review and disposition |
| Work in process | Rework, complete old rev, convert, or scrap | Traveler/lot/operation status |
| Finished old-revision stock | Ship, segregate, rework, or scrap | Customer approval and inventory record |
| Goods in transit | Accept, return, relabel, or replace | Shipment identity and disposition |
| Sub-tier work | Stop, revise, or complete | Controlled communication and acknowledgment |
| Service/spares | Maintain old configuration or transition | Configuration applicability decision |
The person approving disposition must have authority. The supplier cannot convert customer-owned product or ship an old revision merely to avoid waste.
Control Work in Process and Inventory
Run an inventory status report at change receipt. Include raw material committed to the order, staged kits, parts at every operation, inspection holds, rework, finished goods, subcontractor inventory, and shipped product not yet received.
Physically segregate or electronically block affected material until disposition. Labels should show part, revision, lot/work order, quantity, and status. Verify that an operator cannot release quarantined old-revision parts by selecting the wrong ERP status.
Reconcile quantities. If 100 pieces were started, the change record should account for each as converted, accepted at old revision, scrapped, or held. Unexplained balance is a traceability gap.
Update CNC Programs and Setup Documents
A programmer should work from the controlled new master, not patch an old toolpath while leaving its identity unchanged. Record program revision, source model, postprocessor, machine target, verification, and approval.
Review changes to:
- stock and work offset;
- tool list and holders;
- feeds, speeds, and tool-life rules;
- fixtures, jaws, soft jaws, and probing;
- setup sequence and intermediate states;
- in-process measurement and compensation;
- deburring and edge requirements;
- special instructions and visual aids; and
- archived/superseded program access.
The operator interface must show the effective program and part revision. If old and new configurations remain in production, prevent selection by ambiguous file names.
Update Inspection Planning and CMM Programs
Inspection changes may lag manufacturing because attention focuses on the CNC program. Trace new and changed drawing characteristics into the ballooned drawing, inspection plan, gage instructions, CMM program, report template, and acceptance criteria.
Check datum construction, alignments, point strategies, fitting algorithms, tolerance types, units, and material-condition modifiers. A geometry change can require new probe access or fixturing even if the feature’s numeric limit did not change.
Verify the inspection program with an approved method before release. For the first effective lot, require a risk-based first-article or delta inspection that covers changed and potentially affected characteristics. Do not inspect only the visibly revised dimension when a datum or setup change influences other features.
Flow the Change to Purchasing and Subtiers
Suppliers must identify every external provider affected by a revision. That can include material distributors, heat treaters, anodizers, platers, grinders, welders, test laboratories, component suppliers, and packaging vendors.
The flowdown should name the new revision and applicable requirement, attach or link the controlled source, state effectivity, identify old work disposition, and require acknowledgment. Protect customer data according to access restrictions.
Audit one sub-tier response. Confirm receipt date, technical review, updated purchase order, WIP inventory, revised process instructions, and certificate format. A forwarded customer email without a revised order can leave the subcontractor working to old terms.
ISO/IAF guidance for auditing external providers provides useful context for verifying procurement controls. Apply the customer’s product and configuration requirements directly.
Withdraw Obsolete Information at the Point of Use
Updating a master folder is not enough if old files remain on machine controls, shared drives, tablets, printed binders, local desktops, email attachments, inspection stations, or sub-tier portals.
Walk the production route and sample points of use. Ask operators to retrieve the active drawing, program, setup sheet, and inspection instruction without coaching. Verify revision and source. Search for obsolete copies and confirm how access is blocked or their status is marked.
Obsolete records may need retention for traceability, but they should not appear active. Separate archive permissions from production permissions. Read-only archive, watermarking, naming rules, and access control can help.
The ISO guidance on documented information distinguishes information maintained to operate processes from records retained as evidence. That distinction is useful here: current instructions must be controlled at use, while superseded evidence remains retrievable.
Verify Training and Acknowledgment
People affected by the change should understand what changed, when it applies, and what to do with old product. Training need not become a classroom event for every revision; it should be proportionate to complexity and risk.
Evidence might include electronic acknowledgment, shift briefing, updated visual instruction, qualification record, or supervisor verification. Test understanding with a question tied to the real change. A signature alone does not prove that an operator knows how to distinguish old and new configurations.
Cover off-shift and temporary personnel. Changes released during the day can fail on the night shift if handoff relies on one conversation.
Control Digital Repositories and Local Copies
Map where production information can be stored or cached: PLM, ERP, document-management system, CAM vault, machine control, CMM workstation, inspection tablet, network drive, email, and removable media. Define which repository is authoritative for each document type and how users reach it.
Access control should separate approval from use. A programmer may prepare a new file, but release status should prevent an unapproved version from appearing in the production queue. The system should retain revision, approver, effective date, and audit trail. If files are downloaded for machine execution, the transfer needs verification and a method to remove or disable the prior version.
Backups protect availability but can also restore obsolete information. Test how a system recovery preserves current status and prevents old programs from becoming active. For cloud portals, check synchronization failures and offline-device behavior. A tablet that displays last week’s cached drawing during a network outage is a configuration risk.
Restrict USB or uncontrolled file sharing according to security requirements, but keep the production method usable. When an emergency transfer is necessary, record source, checksum or identifier, recipient, target machine, approval, and later cleanup. The audit should follow one file from release to the exact controller or workstation that uses it.
Manage Concurrent Old and New Configurations
Some service, spare, validation, or phased-transition programs legitimately produce two revisions at the same time. The control method must distinguish them throughout scheduling, material issue, machining, inspection, packaging, and certification.
Use separate work orders, travelers, programs, fixture identifiers, storage locations, and labels where risk justifies them. Do not depend on an operator recognizing a subtle model change. Color coding can help visually but should supplement—not replace—positive part and revision identity.
Schedule the configurations to reduce mix risk and document line clearance between runs. Reconcile quantities at every handoff. Inspection reports and certificates must state the actual revision for each lot or serial, and packaging should prevent customer receiving from combining configurations.
When the old configuration finally retires, perform a controlled closeout: account for remaining inventory, complete authorized shipments, archive evidence, remove active programs and instructions, notify subtiers, and update service/spares records. The closeout date is part of the revision history.
Perform First-Effective-Unit Verification
Before normal production release, verify that the first unit or lot under the new effectivity was built from the correct package. Check product identity, route, program, fixtures, material, special processes, and inspection revision.
Define the scope from impact analysis. A change to a hole pattern may require full interface inspection and assembly verification. A new coating may require thickness, masking, appearance, adhesion, and post-coating dimensions. A drawing-note correction may need document confirmation only.
Record actual results and approvals. Link the evidence to the affected serial/lot and change notice. Do not close implementation solely because documents were edited.
Keep Customer and Supplier Approval Distinct
The supplier can review feasibility and propose an implementation date. The customer controls product definition, deviation authority, and acceptance unless the contract delegates them. Identify who may approve:
- interpretation of a drawing conflict;
- use of old revision inventory;
- deviation from a new requirement;
- alternative material or process;
- delayed effectivity;
- partial implementation; and
- acceptance of first revised output.
Meeting minutes may document discussion but may not constitute contractual authorization. Use the approved change or deviation mechanism.
Audit Communications for Clarity
A change notice should answer:
- What exact product and document changed?
- What is the old and new revision?
- Which technical and commercial items changed?
- Which orders, lots, serials, and dates are affected?
- What happens to existing inventory and WIP?
- Which subtiers and internal functions must act?
- Which validation and approval are required?
- Who owns each action and by when?
- What prevents obsolete use?
- How will completion be proven?
Check for ambiguous subject lines, missing attachments, inconsistent file names, and recipients who lack responsibility. A controlled system should not depend on one salesperson remembering every department.
Change-Implementation Evidence Table
| Stage | Evidence | Audit test |
|---|---|---|
| Receipt | Authorized transmittal and intake log | Match source, time, files, IDs |
| Comparison | Change summary or geometry/document comparison | Confirm all changed sources reviewed |
| Impact | Cross-functional assessment | Trace geometry, material, process, inspection, cost, schedule |
| Effectivity | Approved serial/lot/order/date boundary | Reconcile WIP and inventory |
| Planning | Updated router, BOM, PO, tooling, program | Compare active revisions |
| Subtier | Revised order and acknowledgment | Sample external provider implementation |
| Production | Operator-accessible current instruction | Walk point of use |
| Inspection | Updated plan/program/report | Verify changed and affected characteristics |
| Validation | First-effective-unit results | Link evidence to lot and change |
| Release | CoC/packing/ERP revision identity | Match shipped configuration |
| Retention | Superseded archive and audit trail | Retrieve old and new without ambiguity |
Red Flags During a Supplier Audit
- revisions arrive through personal email with no intake log;
- receipt acknowledgment is treated as implementation approval;
- model and drawing identities are not recorded together;
- effectivity says only “next build”;
- WIP and sub-tier inventory are omitted;
- programmers overwrite CNC files under the same uncontrolled name;
- CMM programs have no source drawing/model revision;
- obsolete prints remain beside machines;
- off-shift employees cannot find the new instructions;
- subtiers receive files without revised purchase orders;
- old product ships under a new-revision certificate;
- impact review is always marked “none”;
- exceptions rely on verbal approval; or
- closure proves document edits but not first effective product.
Use each red flag to select evidence and containment. Do not grade only the presence of procedures.
Metrics That Reveal Communication Health
Useful measures include revision acknowledgments on time, open implementation actions, overdue WIP dispositions, first-effective-unit escapes, obsolete-document findings, sub-tier response time, and changes implemented after promised dates.
Define each metric. A fast acknowledgment can be misleading if it means only that an email was opened. Measure the stage that protects production. Review trends and serious individual events; a low average may hide one critical configuration escape.
Connect corrective action to the failed handoff. If operators used an old drawing because the master system was correct but the machine tablet cached a local copy, fixing the title block will not solve the control gap.
Test the Process With a Tabletop Scenario
Before approving a new supplier, provide a controlled hypothetical change based on the proposed part. Ask the team to explain who receives it, how files are compared, what records change, how WIP is found, which subtiers are notified, and how the first new unit is released.
Introduce a complication: half the lot is at anodizing, old finished inventory exists, or the new tolerance affects CMM programming. Observe whether responsibilities and approvals remain clear. The exercise does not prove operational effectiveness, but it reveals missing interfaces worth sampling onsite.
Buyer Pre-Award Checklist
Before award, define:
- authorized change channels and contacts;
- controlling model/drawing/specification hierarchy;
- required acknowledgment stages and timing;
- effectivity format;
- WIP, inventory, and sub-tier disposition authority;
- change-notification and approval thresholds;
- first-article or delta-validation requirements;
- data-security and access rules;
- record retention and retrieval;
- certificate/packing revision identity; and
- response to unauthorized or late implementation.
Ask the supplier to demonstrate one completed change and one obsolete-document search. That evidence is more meaningful than a yes/no questionnaire.
Close the Loop at Shipment
Final release should verify part number, revision, purchase order, lot/serial, quantity, approved deviations, and required records. The Certificate of Conformance, packing list, labels, inspection report, and ERP shipment record should agree.
If old and new revisions ship near each other, use packaging and labeling that prevent mixing at the customer. Communicate split shipments explicitly. Retain the exact released data set and implementation evidence for the agreed period.
After delivery, sample the customer’s receiving record when the relationship permits. Confirm that the revision printed on the supplier’s documents reached the buyer’s system and that attachments remained associated with the right lot. A technically correct factory change can still fail if an ASN, packing list, portal record, or label carries the old revision.
Use any discrepancy to improve the interface, not only the internal procedure. Align field names, file identifiers, portal permissions, and contact lists between organizations. For repeat orders, include the verified configuration in order acknowledgment so that both parties detect a stale purchase order or accidental rollback before material is issued.
For a QuickCNCs repeat-production change, send the controlled new model and drawing, revision summary, effectivity, open-order list, WIP disposition, and validation requirement. We can review machining and inspection impact before committing a release date. The customer’s approved revision and written change authorization remain the product authority.
Tie the revised route to the correct CNC machining services and the verification scope on the quality assurance page. Release the approved change package through Request a Quote.