
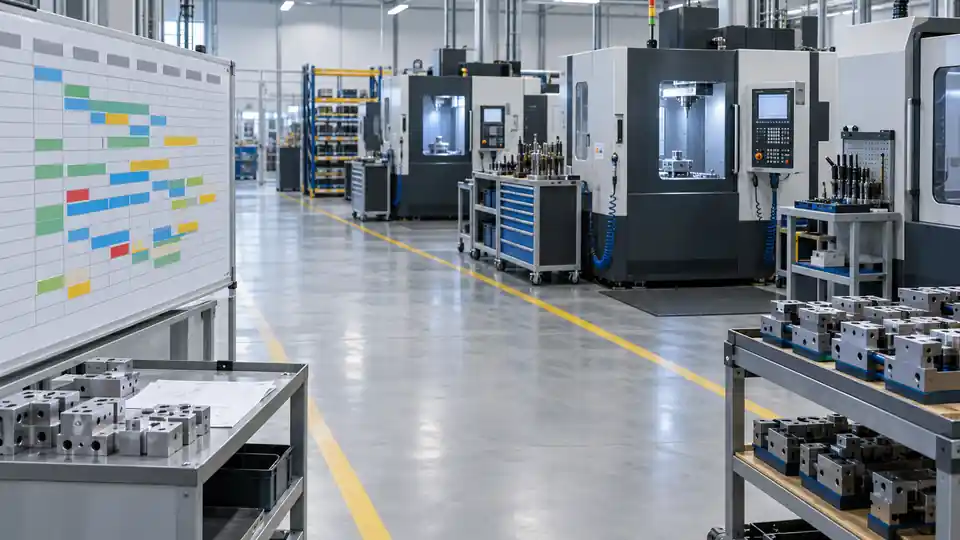
A machine list shows what a CNC supplier owns or can access. It does not show how many qualified hours are available for a new program, which operation controls output, whether trained people cover every shift, or how quickly production can recover from a failure. Capacity must be tested against a defined part family, volume ramp, quality plan, and delivery window.
This CNC supplier capacity audit decision guide turns a broad claim such as “we have plenty of capacity” into evidence a buyer can verify. It explains how to calculate required and available hours, examine bottleneck resources, distinguish demonstrated output from theoretical machine time, expose subcontracting, and stress-test the recovery plan. The goal is not to prescribe how a shop schedules its floor. It is to decide whether the proposed route can meet the awarded demand with credible margin.
Separate Capability From Capacity
Capability asks whether a supplier can make and verify the part. Capacity asks how much conforming product the defined system can deliver in a stated period. A five-axis machining center may have the travel and accuracy for a housing but no available spindle time during the launch month. Conversely, an available three-axis mill is irrelevant if it cannot reach the features or hold the setup relationship.
Evaluate both questions, but do not merge them. First establish the qualified route: machine type and envelope, workholding, tools, programs, special processes, inspection, material, and people. Then evaluate the capacity of that route at the required quality and delivery conditions.
Capacity is time-dependent. The answer for prototype quantities this month may not support a 1,000-piece monthly ramp next quarter. Record the forecast period, required quantity, batch policy, working calendar, and expected mix when asking for evidence.
Build a Part-Specific Demand Model
Translate the commercial forecast into load by operation. Annual volume divided by 12 is rarely sufficient. Launches, promotions, program milestones, shutdowns, and safety-stock builds create peaks. Include the firm window, forecast window, upside scenario, and maximum credible surge.
For each part or representative family, identify:
- pieces required by week or month;
- production lot size and shipment cadence;
- setup frequency and setup duration;
- cycle time by operation;
- expected yield and rework assumptions;
- inspection and special-process time;
- maintenance and planned downtime; and
- changeover or family-mix constraints.
Use approved or demonstrated times where available. If the part has not run, label estimates and state their basis. CAM simulation may estimate cutting time, but it may omit loading, probing, tool changes, deburring, washing, queue, inspection, and normal interruptions.
Convert pieces into required resource hours
For a simple operation, required hours for a period can be framed as:
setup hours + (planned pieces ÷ expected first-pass yield × cycle hours per piece) + inspection or service hours
This is a planning model, not a universal accounting formula. The treatment of scrap, rework, unattended running, and overlapping labor depends on the route. Keep each assumption visible so the buyer can change the forecast and see the load response.
Do not hide a poor yield assumption by loading only the shipped quantity. A process that needs extra starts to produce the order consumes the associated machine, material, labor, and inspection capacity.
Measure Available Hours Realistically
Theoretical calendar time is not available production time. A machine may have 168 hours in a seven-day week, but the shop may staff one shift, reserve weekends for maintenance, or lack night-shift setup and inspection coverage.
Document the calculation for each constrained resource:
| Capacity factor | Evidence to review | Common overstatement |
|---|---|---|
| Scheduled hours | Shift calendar and planned overtime | Counting 24/7 when one shift is staffed |
| Existing load | Finite schedule or order backlog | Showing gross hours before committed work |
| Planned downtime | Preventive-maintenance calendar | Treating maintenance as optional |
| Changeovers | Historical or planned setup time | Counting every hour as cutting time |
| Performance | Actual cycle versus standard | Using best-piece simulation only |
| Quality yield | Scrap and rework by process family | Assuming every start becomes a shipment |
| People | Qualified coverage by shift and role | Counting headcount that cannot run the route |
| Inspection | CMM/gage/program availability | Ignoring release bottlenecks |
| Subtiers | Confirmed slots and lead-time windows | Calling broker access internal capacity |
Available capacity should be shown after committed demand, maintenance, normal variability, and policy reserves. Ask whether the quoted order is already loaded in the supplier’s planning system or merely assumed to fit later.
Find the True Constraint
The machine with the longest cycle is not always the system constraint. A dedicated fixture, large CMM, tool presetter, wash process, approved heat treater, experienced programmer, or final inspector may control throughput. Map the entire release path from material receipt through shipment.
For each step, compare required load with net available time during the same period. Examine queue and batch rules. A short outside process performed only once each week can create more elapsed-time risk than hours of machining.
Look for shared resources. Several machines may all feed one deburring station or CMM. If the supplier displays open spindle hours but does not load inspection, the delivery claim is incomplete.
Constraint migration during ramp
The bottleneck can move as volume increases. Programming and first-article inspection may constrain launch; spindle time may constrain steady production; then final inspection or finishing may constrain the peak. Audit at several demand levels instead of extrapolating one average utilization figure.
Ask the supplier to show the constraint at base demand, forecast peak, and surge demand. The response should state what action is triggered when a threshold is reached.
Audit the Machine List
A credible machine list includes enough detail to connect assets to the proposed route:
- manufacturer, model, machine type, and asset identifier;
- axis travel, spindle, work envelope, and relevant options;
- commissioning year where useful, but not as a proxy for condition;
- current location and ownership or lease status;
- qualification for the part family;
- compatible fixtures, probes, pallets, and automation;
- normal shift assignment and planned maintenance; and
- backup equivalence or requalification work.
Physically verify a risk-based sample during an audit or live video review. Confirm that the machines are installed and operational, not brochure images or planned purchases. Compare asset identifiers with maintenance logs, calibration/verification where relevant, and production scheduling.
Machine age alone is weak evidence. An older machine under disciplined maintenance may be suitable; a new machine without a stable process, qualified operator, or measurement route may not be. Focus on demonstrated performance for similar material, geometry, tolerance, and duty cycle.
Review Actual Loading and Backlog
A percentage such as “70% utilized” needs a denominator, time window, and data source. Ask to see an anonymized finite-capacity schedule, load-versus-capacity report, or other controlled planning output for the constrained resources. Customer names and proprietary details can be masked while retaining dates, hours, and load.
Check whether the report includes released orders, forecast reservations, late work, rework, prototypes, maintenance, and internal jobs. Ask how tentative awards are handled. A supplier may promise the same open slot to several prospects if forecasts are not reserved.
Reconcile schedule data with shop observations. Significant queues in front of a supposedly underloaded resource deserve explanation. Review on-time delivery and backlog age, but do not treat a site-wide average as proof for the route and period you need.
Test the load with a simple reconciliation
Select one recent week for a constrained resource. Compare scheduled hours, recorded run/setup/downtime hours, completed conforming quantities, and remaining work. Differences reveal how accurately the planning system represents reality. The purpose is not an accounting audit; it is to establish whether the capacity promise rests on usable data.
Verify Cycle-Time Evidence
For repeat work, request recent actual cycle-time distributions rather than a single standard. Separate machine cycle, loading, in-process measurement, tool service, part handling, and planned stops. Record batch size and whether multiple parts run per cycle.
For a new part, review the time estimate by operation. Confirm stock size, material, toolpath, tool-change count, probing, work offsets, repositioning, and deburring assumptions. Identify learning-curve allowances and the point at which the quoted standard becomes expected.
One observed fast cycle is not a sustainable rate. Audit across a representative run and include normal tool changes and inspection. If unattended operation is claimed, verify chip control, tool-life monitoring, material loading, alarm response, and the hours during which qualified staff can recover a stop.
Check Tooling and Workholding Capacity
Machines cannot produce without fixtures, toolholders, cutters, gages, and replacement components. Determine whether tooling is dedicated, shared, single-source, or constrained by lead time.
Ask:
- How many fixture sets support the planned lot size and machine count?
- Which items have long procurement or build lead times?
- Are spare inserts, special cutters, jaws, probes, and gages stocked?
- Can the backup machine accept the same fixture and program?
- Who owns customer-funded tooling, and where is it stored?
- How are fixture maintenance and dimensional verification controlled?
A second machine does not provide effective redundancy if only one fixture set exists or a transfer requires weeks of new prove-out.
Evaluate People by Qualification, Not Headcount
Capacity claims often assume that labor can be added immediately. CNC work needs qualified programmers, setup technicians, operators, inspectors, maintenance personnel, and quality decision makers. Skills may be concentrated on one shift or one employee.
Review a skills matrix tied to the proposed route. Confirm coverage for setup, offset changes, abnormal conditions, inspection, and release. Ask about current vacancies, turnover, planned hiring, training time, overtime dependence, and cross-training.
Separate machine attendance from direct labor. One person may monitor several automated machines under stable conditions, but complex setups, frequent part changes, or manual inspection alter that ratio. Night and weekend hours are not available if no one can respond to alarms or approve a restart.
Include Inspection and Quality Release
A shipment is not complete when machining ends. Load the inspection system with first-article programming, in-process checks, final inspection, document review, and nonconformance handling.
For CMM-intensive work, examine machine envelope, probe access, program-development time, qualified operators, fixture availability, and schedule by shift. For manual gaging, confirm enough dedicated instruments and that calibration/verification does not create a hidden queue.
Quality problems consume capacity twice: they create replacement machining and additional investigation or inspection. Review first-pass yield, rework, scrap, and concession rates for a comparable process family. Do not deduct all historic quality losses as though they will disappear on the new program.
Expose Outside Processing and Material Constraints
An internal machine schedule cannot compensate for unavailable material, heat treatment, plating, anodizing, grinding, nondestructive testing, or transport. List every external step, approved source, normal lead time, batch cadence, minimum charge, capacity reservation, and backup.
Ask for evidence of current sub-tier commitments when an outside process lies on the critical path. A supplier saying “we have several vendors” is weak if the customer approves only one or if the alternatives lack the required process class.
Material should be modeled by exact grade, form, size, condition, certification, and lot policy. Generic stock availability is not proof for a large custom billet or controlled heat. Review supplier quotes, committed allocations, safety stock, and substitution authority.
ISO/IAF Auditing Practices Group guidance on external providers offers useful context for evaluating how externally provided processes are controlled. The buyer still needs product-specific evidence for the awarded route.
Distinguish Strong Evidence From Weak Evidence
| Claim | Weak evidence | Stronger evidence |
|---|---|---|
| “We have four suitable mills” | Website machine list | Asset list plus route mapping, qualification, schedule, and backup conditions |
| “Capacity is 40% open” | Verbal percentage | Net-load report with denominator, period, existing commitments, downtime, and yield |
| “We can add a second shift” | Hiring intention | Named staffing plan, skills coverage, training dates, and supervision |
| “Cycle time is 20 minutes” | CAM screenshot | Representative run data including loading, tool service, and inspection effects |
| “Inspection will not delay release” | CMM model name | Load plan, program status, fixture/probe coverage, qualified operators, and queue data |
| “Finishing is covered” | List of vendors | Approved source, quotation, reserved slot, transport, yield, and backup |
| “Another machine is backup” | Similar machine model | Fixture/program compatibility and defined revalidation plan |
| “We recover quickly” | Generic continuity policy | Part-specific trigger, owner, alternate route, materials, tooling, and tested timing |
Evidence should be recent, traceable, and representative. A successful unrelated aluminum bracket does not establish output for a tight-tolerance stainless-steel housing.
Audit Ramp Capacity, Not Only Steady State
Launch work adds programming, fixture prove-out, first article, corrective changes, and approval queues. A supplier may have adequate steady-state hours but insufficient engineering and inspection bandwidth for several concurrent launches.
Build a ramp table showing weekly quantity, required resource hours, qualification milestones, material arrival, outside-process slots, and customer approvals. Identify the first date on which the full rate is demonstrated rather than assumed.
Use rate-readiness reviews at defined gates: process design, tooling complete, first article, pilot lot, rate demonstration, and production release. Each gate should have evidence and an owner. Do not call a machine “available” while it is still awaiting fixture, program, gage, or customer approval.
Stress-Test the Promise
A capacity plan with no upset scenario is fragile. Test plausible events:
- the constraint machine loses a spindle for one week;
- the sole programmer or inspector is unavailable;
- material arrives late or one heat is rejected;
- the finishing source misses its slot;
- first-pass yield is lower than planned;
- demand moves forward or increases;
- another major customer accelerates orders; or
- the backup machine needs requalification.
For each scenario, quantify lost hours or pieces, inventory coverage, recovery action, alternate route, approval required, and time to return to schedule. Avoid a list of generic risks without arithmetic.
Recovery may use overtime, alternate equipment, split lots, safety stock, qualified subtiers, or customer-approved sequence changes. Identify limits: overtime cannot repair an unavailable special process, and outsourcing cannot bypass approval or intellectual-property controls.
Check Maintenance and Reliability
Review preventive-maintenance completion, unplanned downtime, mean time to repair where tracked, critical spares, service support, and escalation for constrained equipment. Look at records for the actual assets proposed.
A supplier should not need perfect reliability. It should understand failure patterns and have proportionate controls. Chronic alarms, overdue maintenance, or unavailable replacement parts can invalidate nominal open hours.
Ask when maintenance is loaded into the production schedule and how a delayed task is approved. Verify that running extra shifts does not silently consume planned maintenance time.
Review Change and Allocation Rules
Capacity can erode after award. The supplier may add customers, move work, pool machines, change subtiers, or reallocate people. Define which changes require notification or approval.
For high-risk programs, agree:
- forecast update frequency and firm horizon;
- reserved capacity and cancellation rules;
- allocation priority during constraints;
- trigger points for added tooling or equipment;
- notice for route, site, machine family, or sub-tier changes;
- rate reporting and recovery communication; and
- ownership of dedicated assets and safety stock.
Commercial commitments should align with the evidence. Paying for a reservation without defining the reserved resource and period provides little protection.
Keep Capacity Evidence Current
Capacity findings age quickly. A machine-load report, staffing roster, or sub-tier quotation that supported award can become obsolete after a large new order, equipment failure, resignation, or forecast change. Put an as-of date on every major evidence item and define the event or interval that triggers refresh.
During production, monitor a small set of forward-looking measures rather than waiting for a missed shipment. Useful signals include constrained-resource load for the firm horizon, past-due hours, queue age, first-pass yield, unplanned downtime, open quality holds, material coverage, outside-process turnaround, and staffing gaps. Each measure needs a definition, data owner, review frequency, and escalation threshold.
Reconcile forecasts with actual releases. If the buyer regularly orders above the stated forecast, the original supplier commitment may no longer describe the demand. If the supplier accepts new work that consumes reserved hours, the buyer needs early notice and a recovery proposal. Capacity governance works only when both sides maintain the assumptions they approved.
Evidence freshness should be proportional to risk. A low-volume prototype may need a focused pre-award check. A production ramp around a single constrained asset may justify weekly load reviews until the rate stabilizes. Avoid requesting a large dashboard that no one uses; retain the few measures that directly predict whether the next delivery window is protected.
Capacity Audit Scorecard
Use a scored assessment only after reviewing the underlying evidence. A practical scorecard can rate:
- demand definition and forecast alignment;
- route and bottleneck identification;
- cycle-time basis;
- finite loading and backlog accuracy;
- equipment availability and maintenance;
- tooling and workholding readiness;
- skilled staffing by shift;
- inspection and release capacity;
- material and sub-tier commitments;
- launch/ramp readiness;
- recovery and alternate-route maturity; and
- change control and reporting.
For every low score, record the action, owner, evidence due, and timing effect. Do not average away a critical single-point failure with high scores on less important sections.
Red Flags That Need Follow-Up
- utilization is quoted without a period or denominator;
- capacity equals total calendar hours;
- only spindle time is modeled;
- the machine list cannot be tied to the proposed route;
- a planned equipment purchase is treated as installed capacity;
- existing backlog is omitted;
- cycle time comes only from an ideal simulation;
- night/weekend output lacks qualified coverage;
- inspection and outside processes are absent from the load model;
- several “backup” machines share one fixture, program expert, or CMM;
- quality losses are assumed to be zero;
- new awards are not entered into a finite schedule;
- contingency actions have no quantified recovery time; or
- the supplier refuses even anonymized scheduling evidence.
One red flag is not automatic disqualification. It identifies uncertainty that should be closed before the buyer relies on the claim.
Supplier Evidence Request
Before award, request a concise package containing:
- part-family route and operation list;
- demand profile and upside scenario;
- cycle/setup/inspection assumptions;
- required hours by constrained resource;
- net available hours after current commitments;
- anonymized schedule or load report;
- machine and critical-tooling identifiers;
- skills coverage by shift;
- material and outside-process commitments;
- launch milestones and rate demonstration;
- first-pass-yield and downtime basis for comparable work;
- recovery scenarios and alternate-route conditions; and
- unresolved assumptions, actions, owners, and dates.
The NIST MEP supply-chain program describes supplier evaluation, supply-chain mapping, risk assessment, total cost of ownership, and supplier development as connected activities. That broader view fits a capacity audit: apparent machine hours matter only within the complete delivery system.
Make the Award Decision on Net, Demonstrated Capacity
A credible supplier can explain the demand model, proposed route, true constraint, net available hours, staffing, inspection, sub-tier dependencies, and recovery limits. The evidence will contain assumptions and uncertainty; the key is that they are visible and tied to actions.
For a QuickCNCs capacity review, provide the controlled model and drawing, quantities by period, lot and delivery cadence, critical quality requirements, and ramp timing. We can return a route-specific quotation and capacity discussion. Buyers should preserve the agreed assumptions in the purchase order or quality plan and update them when demand or process scope changes.
Compare the proposed bottleneck with the relevant CNC machining services route and, for variable demand, the low-volume CNC machining approach. Submit the time-phased demand and recovery assumptions through Request a Quote.