
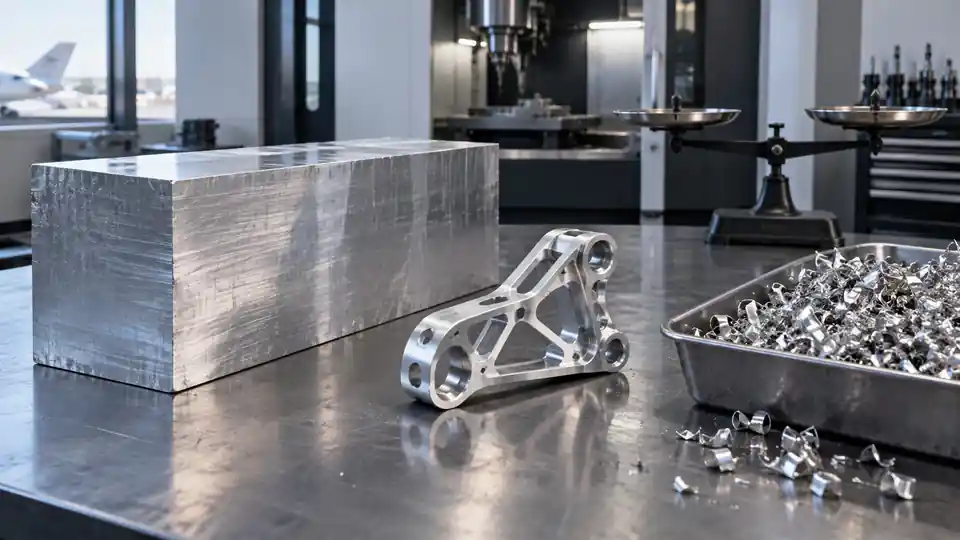
A CNC quote is affected by the material that becomes the part and by everything purchased only to be cut away. Buy-to-fly ratio compares the mass of starting stock with the mass of the finished component. A ratio of 8:1 means eight units of raw-material mass are purchased for every one unit that remains in the accepted part. The other seven become chips, saw loss, qualification pieces, machining allowances, or unusable remainder.
The ratio is most familiar in aerospace manufacturing, but the principle applies to any plate-machined housing, bracket, manifold, optical mount, or contoured component. A high ratio can raise raw-stock cost, roughing time, tool consumption, coolant load, handling, distortion risk, and the amount of cash committed before a good part exists.
Buy-to-fly is not a quality score. A high ratio can be the correct choice for a prototype, a safety-critical part, or a design that needs uninterrupted grain structure. A lower ratio can require expensive near-net tooling, minimum buys, long lead time, or a process that is unsuitable for the required tolerance. This guide shows how to use the metric in a quote without turning it into a misleading target.
How to Calculate Buy-to-Fly Ratio
Use consistent mass units:
Buy-to-fly ratio = purchased starting-stock mass ÷ finished-part mass.
If the blank weighs 12 kg and the finished part weighs 2 kg, the ratio is 6:1. Material utilization is the inverse:
Material utilization = finished-part mass ÷ purchased mass × 100%.
The same example has 16.7% utilization. These calculations are simple; deciding which mass belongs in the numerator is not.
Define the starting-stock boundary
For one part cut from an individual billet, use that billet’s purchased mass. For several parts nested in plate, allocate the plate mass across the accepted parts and account for skeleton, edge trim, test coupons, and unusable remainder. If a bar remainder will be used on another order, agree whether the quote charges the full length, allocates actual consumption, or credits reusable stock.
Include saw kerf, facing allowance, and clamping stock. Do not calculate from the finished part’s bounding box and call it the purchased blank unless the supplier can actually obtain that exact size.
Use the correct finished mass
Calculate the accepted part in its final design state. If coating, inserts, or assembled items materially affect mass, state whether they are included. For geometry at an early revision, mark the ratio as preliminary and update it when the model stabilizes.
Density in the CAD system must match the specified material. A generic “aluminum” or “steel” density can distort mass comparison. For a rough quote, volume ratio may be used when the stock and part are the same homogeneous material, but mass is clearer when materials or inserts differ.
Buy-to-Fly Is Different from Nesting Yield
Buy-to-fly measures starting mass relative to part mass. Nesting yield describes how efficiently profiles or blanks fit within plate, sheet, bar, or another purchased form. They interact but are not identical.
A flat bracket can have good nesting yield yet still require extensive pocketing, creating a high buy-to-fly ratio at the machined-part level. A solid block may have a modest ratio but poor purchasing yield if the supplier must buy a full plate for one small blank. Keep these losses separate:
- mill or distributor minimum buy;
- plate/bar nesting and saw loss;
- blank-to-finished-part material removal;
- setup scrap, test pieces, and process allowance;
- remainder that cannot be reused economically.
This breakdown tells the buyer which change could help. Rotating a part in plate may improve nesting; changing a deep pocket may reduce machining removal; choosing a standard thickness may avoid a full custom mill order.
Why Stock Must Be Larger Than the Part
The starting blank needs enough material to clean up and provide reliable workholding. Quoters consider:
- incoming thickness, width, length, straightness, and flatness tolerances;
- saw or waterjet accuracy and heat-affected or rough edges where relevant;
- scale, decarburization, surface damage, or mill finish to be removed;
- clamping tabs, chucking length, and fixture access;
- facing allowance to create datums;
- distortion and stress-relief stock;
- grinding, honing, heat-treatment, or coating allowance;
- part orientation and grain-direction restrictions;
- probing and first-off verification needs.
A CAD bounding box equal to the nominal part size will rarely be a safe purchasing size. If the quote assumes too little allowance, the billet may not clean up. If it assumes a very conservative allowance, material and cycle cost are inflated. Ask the supplier to identify its proposed stock form and nominal purchased size.
How a High Ratio Changes Material Cost
Raw-material cost is approximately purchased mass multiplied by effective cost per mass, plus cutting, certification, freight, and minimum-order effects. The effective rate may increase for unusual alloy, temper, thickness, size, melt route, approved source, or traceability.
At a high buy-to-fly ratio, a small change in stock price has a large effect on each part because most purchased material does not remain in the product. That is especially important for titanium, nickel alloys, copper alloys, high-grade stainless, certified aerospace plate, and engineered polymer shapes.
Ask whether the quote includes:
- full plate/bar purchase or allocated consumption;
- distributor cut charge;
- certificate or mill-report cost;
- minimum order quantity;
- price validity and commodity surcharge;
- reusable remnant credit;
- scrap or chip recovery credit;
- material reserved for setup or destructive testing.
Material price alone does not explain the quote. A more expensive near-net form can reduce machine time and risk enough to lower total cost.
Roughing Time and Material-Removal Rate
Removed volume must be converted into chips. Roughing time depends on material removal rate, but a quote cannot safely use one catalog value across the entire part. Machine power and torque, spindle speed, tool engagement, flute capacity, coolant, chip evacuation, rigidity, tool reach, corner conditions, and material behavior all limit the practical rate.
The calculation framework is:
Approximate roughing time = removed volume ÷ sustainable average material-removal rate, plus noncutting time.
Noncutting time includes positioning, tool changes, entry/exit, probing, clearing chips, repositioning, and load/unload. A high theoretical rate in an open pocket may not apply near thin walls, deep corners, or interrupted cuts.
Do not demand a shop’s confidential speeds and feeds. Ask whether the high-removal features dominate cycle time, which geometry restricts tool diameter or reach, and whether a different stock form or design would change the route.
Tooling, Coolant, and Chip Management
High material removal consumes cutting edges and machine resources. Tool cost depends on material, cutter diameter, engagement, reach, coating, tool life, and change strategy. Chips must be evacuated without recutting, packing a cavity, damaging the surface, or blocking coolant.
Deep aluminum pockets can generate large chip volume even when the material cuts quickly. Titanium and nickel alloys may generate less volume per time but impose high heat and tool-wear demands. Abrasive filled polymers create a different wear and dust-management problem.
At production volume, the supplier may invest in optimized roughing tools, high-pressure coolant, through-spindle delivery, chip conveyors, or process monitoring. At prototype volume, the most efficient industrial solution may not amortize. Quantity belongs in the buy-to-fly discussion.
Residual Stress and Distortion
Removing most of a billet changes its stiffness and can release residual stress. A part may move during roughing, after unclamping, during heat treatment, or after finishing. The risk depends on alloy and temper, product form, material-removal balance, geometry, wall thickness, fixture force, thermal input, and sequence.
A high ratio is not the sole cause of distortion, but it can be a warning signal. Large pockets cut from one side of plate, thin frames, and asymmetric ribs deserve a staged process. Options may include:
- stress-relieved stock condition;
- balanced removal from opposite faces;
- roughing with finish allowance;
- unclamp-and-rest or thermal stabilization;
- intermediate stress relief when allowed;
- low-distortion workholding;
- finish machining from functional datums;
- inspection in a defined free or restrained state.
These operations add time. If the drawing requires tight flatness after heavy removal, the quote should show the stabilization and inspection assumption rather than hiding it in scrap risk.
Stock Form Options
Standard plate, bar, and billet
Standard wrought stock is flexible, widely available for many alloys, and suitable for prototypes and revisions. It may create high removal but avoids custom tooling. Certified stock can often be sourced with clear heat/lot evidence.
Custom extrusion
An extrusion can place material near the required cross-section, reducing removal for long prismatic parts. It introduces die cost, minimum order, extrusion tolerance, straightness, grain flow, available alloys/tempers, and mill lead time. Secondary machining is still needed for precise features.
Forging
A forging can improve material utilization and create favorable grain flow for structural components. Tooling, qualification, draft, flash, machining datum strategy, and minimum quantity matter. A near-net forging is not automatically dimensionally stable or ready for minimal inspection.
Casting
Castings can reduce machining volume for complex housings and manifolds. The design must address porosity, inclusions, wall uniformity, draft, datum targets, sealing surfaces, pressure integrity, and inspection. Tooling and validation can make casting unsuitable for early prototypes but attractive at stable volume.
Additive preform
Additive manufacturing can create near-net geometry for expensive alloys or complex internal structures. It introduces build orientation, support removal, surface condition, anisotropy, heat treatment, internal quality, qualification, and finish-machining stock. Compare the complete qualified route, not only material utilization.
Welded or assembled construction
Splitting a monolithic part into joined components can reduce starting mass. It also adds welds, fasteners, seals, distortion, tolerance stack, corrosion interfaces, cleaning, and inspection. Use this route when assembly function supports it, not merely to improve a ratio.
An Illustrative Quote Comparison
Assume a finished aluminum component has a CAD mass of 1.5 kg. These hypothetical routes show how the calculation is used; they are not price or process claims.
| Route | Purchased mass per part | Buy-to-fly | Main cost considerations |
|---|---|---|---|
| Standard plate billet | 10.5 kg | 7.0:1 | available stock, high roughing volume, flexible for revisions |
| Optimized nested plate | 8.4 kg allocated | 5.6:1 | better nesting, saw plan, shared plate, remnant control |
| Custom extrusion | 4.2 kg allocated | 2.8:1 | die/NRE, minimum buy, extrusion tolerance, reduced roughing |
| Near-net forging | 3.0 kg allocated | 2.0:1 | forging tooling, qualification, machining allowance, volume commitment |
The lowest ratio does not automatically win. For five prototypes, plate may have the lowest total cost and shortest lead time. For stable annual demand, extrusion or forging may repay its nonrecurring investment. The decision depends on actual supplier quotes, not the ratio alone.
Include Chip Recovery Correctly
Metal chips can have recycling value, but gross weight multiplied by a commodity price is not a valid automatic credit. Chip value depends on alloy segregation, contamination, coolant, moisture, transport, market, and who owns the scrap under the commercial agreement.
Keep alloys separated where recovery is important. Mixed aluminum, stainless, titanium, and steel chips lose value and can create traceability concerns. Some regulated or customer-owned material may have destruction or return requirements.
Ask whether scrap recovery is already included in the quote and avoid double counting. For expensive alloy at production scale, a transparent chip-ownership or credit rule may be worthwhile. For a small prototype, administration and transport may exceed the recoverable value.
DFM Changes That Reduce Removal
Evaluate geometry with function first:
- reduce unnecessarily thick floors, walls, or bosses;
- open pockets where assembly and sealing allow;
- replace deep solid sections with ribs;
- standardize wall thickness for more balanced removal;
- increase internal corner radii to allow larger roughing tools;
- split a part only when the joint is functionally acceptable;
- align the design with a standard bar, plate, or extrusion size;
- permit a stock surface on a nonfunctional area when appropriate;
- revisit grain-direction restrictions that lack a design basis;
- consolidate several variants into a common preform if volume supports it.
Do not thin a part solely to improve material utilization. Recheck stiffness, fatigue, impact, sealing, vibration, thermal behavior, corrosion allowance, fastener loads, and manufacturing distortion. The supplier can propose material and process alternatives; engineering approves the design change.
The QuickCNCs 5-axis CNC machining page is relevant when better tool orientation can shorten reach or combine setups. It may reduce time and risk even when starting mass does not change.
Compare Quotes with a Material-Flow Map
Ask each bidder to document a high-level flow:
- specified grade, temper/condition, and product form;
- purchased stock size and mass;
- blank cutting and nesting allocation;
- rough-machining and stabilization stages;
- finish machining and special processes;
- accepted finished mass;
- expected remainder and chip treatment;
- certification and traceability boundary.
Then compare these items on the same table:
| Quote input | Supplier response | Buyer check |
|---|---|---|
| Purchased stock | form, size, condition, source assumption | Will the billet clean up and meet the material specification? |
| Allocation | full buy, per-part use, or nested share | Are minimum buy and reusable remainder treated consistently? |
| Ratio | starting mass divided by finished mass | Are both masses based on the same revision and density? |
| Roughing | dominant removal features and process | Is cycle-time risk visible without demanding proprietary feeds? |
| Stability | stock condition and process sequence | Does the route address heavy or asymmetric removal? |
| Alternatives | standard stock, nesting, extrusion, forging, casting | What quantity and validation make each option economic? |
| Recovery | chip ownership/credit and segregation | Is credit already included and commercially realistic? |
Prototype and Production Decisions
For prototypes, prioritize available stock, short lead time, revision flexibility, and enough allowance to obtain a good part. Record the actual blank so a later production comparison starts from evidence.
For pilot builds, improve nesting, validate material behavior, measure roughing time, and identify distortion. Consider modular fixtures and standard stock before committing to a dedicated preform.
For production, compare annual purchased mass, machine capacity, tooling, scrap, working capital, and supply continuity. A near-net form may reduce recurring cost but create a single-source die or long replenishment time. Qualify backup stock or an alternate route where business continuity matters.
The QuickCNCs production CNC machining page provides the manufacturing context for repeat work. The RFQ still needs forecast quantity, release size, revision maturity, and material evidence.
Run a Sensitivity Check Before Redesigning the Part
A ratio can look dramatic while the economic opportunity is small, or look ordinary while expensive certified stock makes it important. Test the variables separately.
Start with the current quote and ask how total cost changes under these controlled scenarios:
- the same geometry nested more efficiently in standard stock;
- the same part in the next available stock thickness;
- a modest DFM change that reduces the blank envelope;
- a larger batch that uses a full plate or bar more efficiently;
- an alternate near-net route with its tooling and minimum quantity;
- a material price increase or a longer procurement lead time;
- no chip credit versus the supplier’s documented recovery treatment;
- a design revision that makes committed custom stock obsolete.
Keep geometry, material grade, certification, finish, inspection, and delivery constant unless the scenario explicitly changes them. Otherwise, the comparison mixes buy-to-fly improvement with a different product requirement.
Separate mass savings from time savings
Removing one kilogram from the purchased blank does not guarantee the same reduction in chips. It may simply reduce a saw edge or clamp allowance. Likewise, a lower-ratio preform may still need slow finishing over the same critical surfaces. Ask for material and cycle effects separately:
Material opportunity = change in allocated purchased mass × effective material cost, adjusted for minimum buys and recovery.
Machining opportunity = change in sustainable cutting and noncutting time × quoted process cost, adjusted for tooling and qualification.
These are supplier-specific inputs. The equations organize the decision; they do not create a market price.
Include the cost of a bad blank decision
An undersized blank that fails to clean up can lose the raw material, completed machining time, outside processing already performed, and schedule slot. An oversized blank usually costs more but may provide process margin. The responsible goal is the smallest verified blank for the approved route—not the smallest theoretical box around the model.
For a repeat job, retain evidence about actual cleanup, stock variation, fixture grip, distortion, and yield. That permits a controlled reduction in allowance after the process demonstrates margin. Do not shrink stock from one successful prototype without considering the incoming material tolerance and the full production distribution.
Track a Small Set of Production Metrics
If the ratio materially affects cost, track metrics that can be acted upon:
- purchased mass and accepted finished mass by revision;
- plate/bar yield and reason for unusable remainder;
- removed volume and actual roughing time;
- tool consumption in the dominant removal operations;
- scrap attributed to material cleanup, distortion, or other causes;
- recovered chip mass and documented commercial treatment;
- first-pass yield after any stock-form or DFM change;
- inventory and obsolete material tied to minimum buys.
Review trends at the process-change boundary. If a new fixture improves nesting but scrap rises because parts move during roughing, the total result is worse. If a custom extrusion lowers removal but introduces long supply interruptions, the continuity plan must be included. The metric set should support a decision, not become a reporting exercise.
Buy-to-Fly RFQ Checklist
Before requesting a quote, provide:
- controlled 3D model with correct material density;
- 2D drawing and matching revision;
- material grade, condition, product form, and certification;
- part orientation or grain direction when required;
- prototype, batch, and annual quantities;
- finishing and heat-treatment sequence;
- tight flatness, thin-wall, or distortion-sensitive requirements;
- permission or limits for alternate stock forms;
- traceability, scrap ownership, and customer-owned material rules;
- delivery cadence and design-maturity information.
Ask the supplier to identify purchased stock size, mass allocation, major machining stages, material minimums, and any DFM alternative. Do not prescribe an unverified blank size in the RFQ if the supplier is responsible for process planning.
Use the Ratio to Ask Better Questions
CNC material removal ratio cost is useful when it exposes where money and risk enter the process. It should prompt questions about stock form, nesting, allowance, roughing, stability, and volume. It should not become a target that pushes the team into premature tooling or an unsuitable near-net process.
To obtain a comparable quotation, send the controlled model, drawing, quantity, material, finish, inspection, and delivery requirements through the Request a Quote page. Ask for the proposed starting stock and assumptions. A supplier can then show whether the best improvement is better purchasing yield, more efficient machining, a DFM change, or a different manufacturing route—and engineering can approve the change without losing the functional baseline.